1. What Is Ammonium Bicarbonate?
Ammonium bicarbonate is a common inorganic compound with the chemical formula NH₄HCO₃. It usually appears as a white crystalline or powdered solid, is readily soluble in water, and has a characteristic ammonia-like odor.
It is widely used in agriculture, food processing, chemical manufacturing, and various industrial processes.
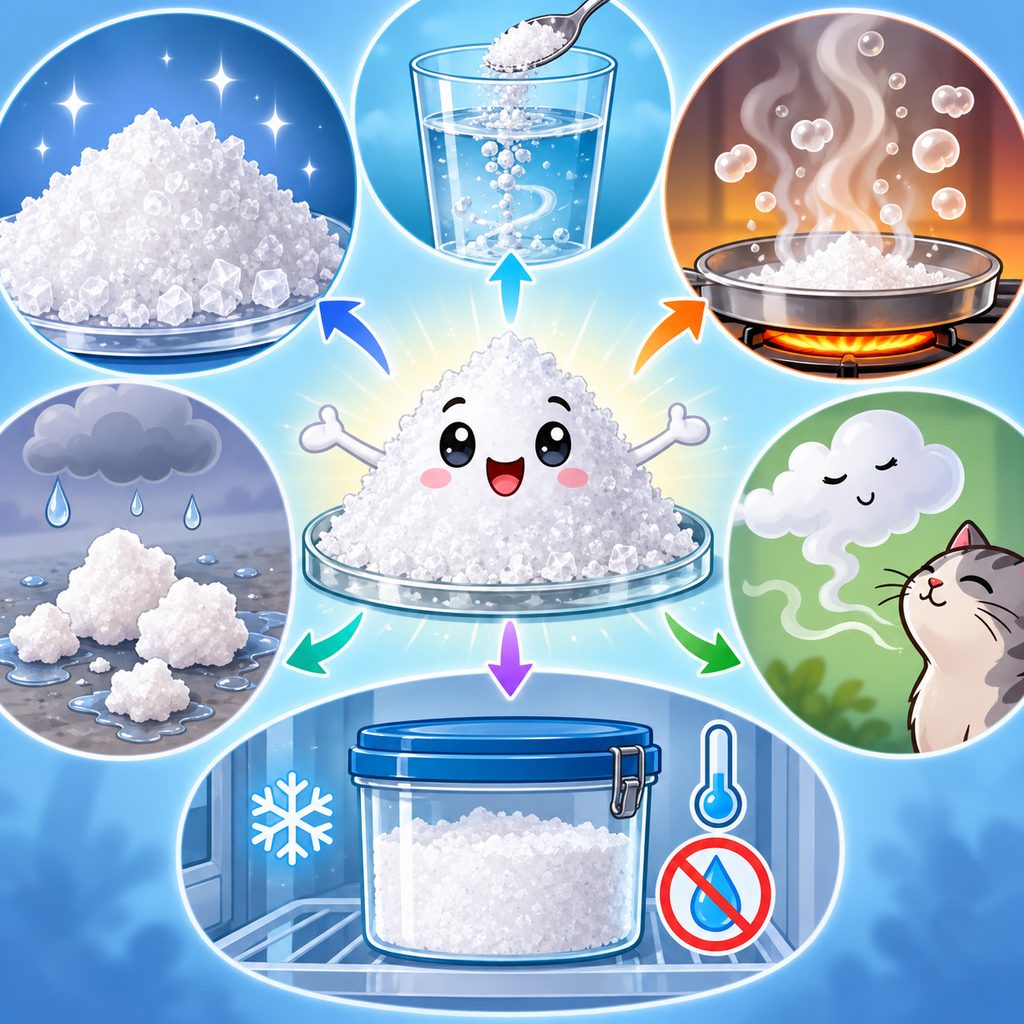
Compared with many chemically stable bulk solids, ammonium bicarbonate has one important characteristic: it is sensitive to heat and can decompose when the temperature rises.
During thermal decomposition, ammonium bicarbonate releases ammonia, carbon dioxide, and water. For this reason, storage temperature, ventilation, sealing conditions, material handling, and instrument installation must all be considered when designing an ammonium bicarbonate storage system.
For plants that store ammonium bicarbonate in silos, bins, hoppers, or intermediate storage vessels, monitoring the material level is also an important part of process automation.
Reliable high-level and low-level detection helps operators prevent overfilling, maintain continuous material supply, and improve the overall reliability of the production process.
Therefore, selecting a suitable ammonium bicarbonate level switch is an important part of bulk solids handling system design.
2. What Is Ammonium Bicarbonate Used For?
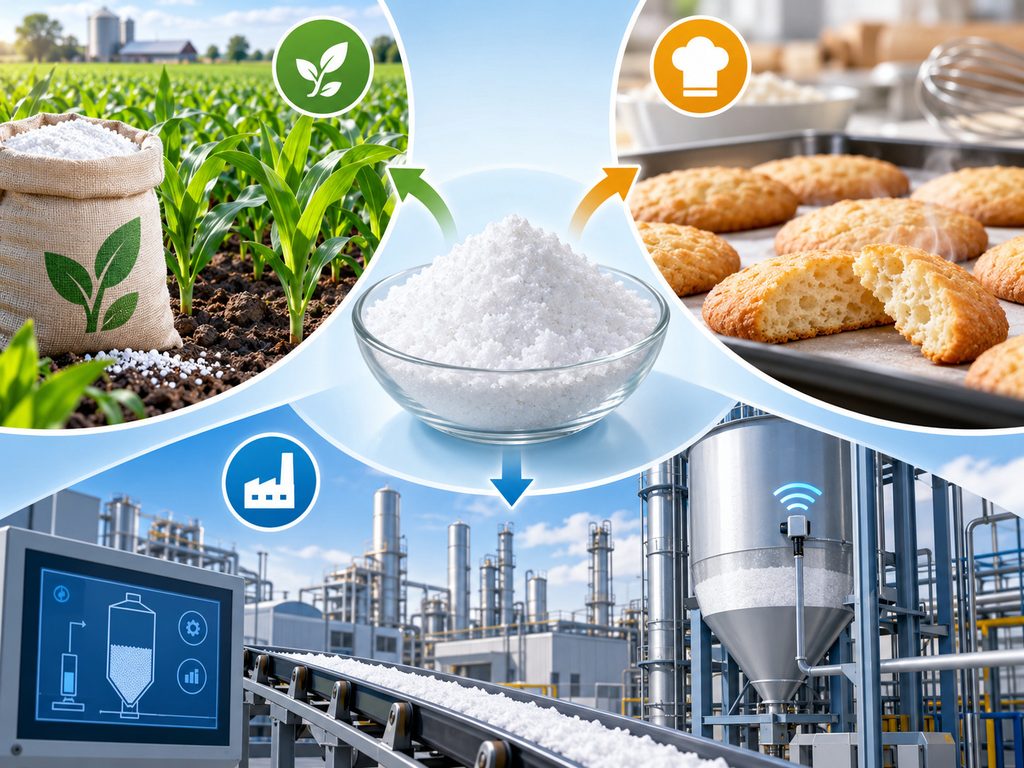
Ammonium bicarbonate has a wide range of applications. Requirements for purity, particle size, packaging, and storage conditions may vary depending on the industry.
2.1 Agriculture
Ammonium bicarbonate is a nitrogen-containing compound that can be used as a nitrogen source in agricultural applications.
Because the material has a certain degree of volatility and is sensitive to environmental conditions, proper sealing, temperature control, and storage management are usually required to minimize the loss of active components.
2.2 Food Processing
Food-grade ammonium bicarbonate is used in certain baked products as a leavening agent.
When heated, it decomposes and releases gases that help create a porous or expanded structure in the food product.
The use of ammonium bicarbonate in food production must comply with applicable food safety regulations and local standards for food additives.
2.3 Chemical Processing
In the chemical industry, ammonium bicarbonate can be used as a raw material, intermediate material, or process additive.
Many chemical plants therefore use ammonium bicarbonate silos, day bins, storage hoppers, or weighing systems to supply the material to downstream equipment through automated conveying systems.
In these applications, reliable powder level detection is often required to support material handling and process control.
3. Key Storage Characteristics of Ammonium Bicarbonate
When selecting a level switch, knowing only the name of the material is not sufficient.
The performance of a level detection device depends largely on how the material behaves under actual process conditions.
For ammonium bicarbonate storage, several characteristics deserve particular attention.
Temperature Sensitivity
Ammonium bicarbonate is sensitive to temperature.
As the temperature increases, its decomposition rate can increase, potentially releasing ammonia, carbon dioxide, and water.
Before selecting a level switch, it is therefore important to determine both the normal operating temperature and the highest possible process temperature inside the silo or hopper.
Instrument selection should not be based solely on ambient temperature.
Potential heat sources may include:
- Warm conveying air
- Process heat transferred from nearby equipment
- Solar heating of outdoor silos
- Seasonal high temperatures
- Heat generated by upstream or downstream processes
The selected level switch should have a process temperature rating suitable for the actual operating conditions.
Dust Generation During Material Handling
Ammonium bicarbonate in powder or fine granular form may generate dust during filling, discharge, pneumatic conveying, screw conveying, or other material handling operations.
Dust concentration may become particularly high near the silo filling point.
If a high-level switch is installed too close to the inlet, both falling material and suspended dust may affect the sensor.
Therefore, the level switch should be suitable for dusty environments, and the installation position should be selected carefully to avoid unnecessary interference.
Caking and Material Build-Up
Moisture can significantly change the physical behavior of powdered materials.
When ammonium bicarbonate is exposed to humid conditions, the material may become sticky, form lumps, or develop deposits on the silo wall or sensing element.
Over time, material that initially flows freely may form larger agglomerates.
For a point level switch, this can become an important reliability issue.
Material build-up on a sensing probe may cause some detection technologies to incorrectly indicate that material is still present.
For this reason, when selecting a level switch for ammonium bicarbonate, resistance to material build-up and long-term operating stability can be more important than simply choosing the highest possible sensitivity.
4. Why Does an Ammonium Bicarbonate Silo Need a Level Switch?
A level switch is designed to detect whether material has reached a specific point.
Unlike a continuous level transmitter, which measures the changing level throughout the vessel, a point level switch provides a discrete switching signal at a predetermined position.
In ammonium bicarbonate storage systems, level switches are commonly used for the following functions.
High-Level Alarm
When the material reaches the designated high-level position, the switch sends a signal to the control system.
The system can then stop filling or alert operators, helping reduce the risk of silo overfilling and material overflow.
High-High Level Protection
For critical storage vessels, an independent high-high level switch may be installed in addition to the normal high-level alarm.
This provides an additional layer of overfill protection.
Low-Level Alarm
A low-level switch detects when the material falls below a specified point.
The signal can be used to initiate replenishment or notify operators before the downstream process runs out of material.
Low-Low Level Protection
A low-low level switch can provide additional protection for downstream equipment.
For example, it can help prevent screw conveyors, feeders, dosing systems, or other equipment from operating for extended periods without material.
In modern automated plants, level switches are therefore used not only to determine whether material is present but also as part of process interlocks and equipment protection systems.
5. What Should Be Considered When Selecting an Ammonium Bicarbonate Level Switch?
Selecting the correct level switch requires an understanding of both the material and the process.
The following factors should be evaluated before determining the appropriate detection technology.
5.1 Confirm the Material Form
The first step is to determine whether the ammonium bicarbonate is stored as a fine powder, crystalline material, granules, or material that tends to form lumps.
Even when the chemical composition is identical, differences in particle size, moisture content, bulk density, and compaction can significantly affect flow behavior.
Therefore, a level switch should not be selected based only on the material name.
Before selecting the instrument, it is recommended to provide information such as:
- Material name
- Powder or granular form
- Approximate particle size
- Bulk density
- Moisture content
- Tendency to cake
- Tendency to adhere or build up
The more complete the process information, the more accurate the level switch selection can be.
5.2 Evaluate the Dust Level
If ammonium bicarbonate is transferred through pneumatic conveying, rapid top filling, or a filling system with a large drop height, significant dust may be generated inside the silo.
In this situation, the level switch should be capable of operating reliably in dusty conditions.
High-level switches deserve particular attention because they are often located close to the filling area.
Whenever possible, the sensor should not be installed directly in the falling material stream.
5.3 Consider Caking and Build-Up
Caking is an important consideration in powder level measurement.
If the silo has relatively high humidity or the material remains in storage for an extended period, ammonium bicarbonate may gradually form lumps or deposits.
Material can also accumulate around the sensing element.
When comparing level detection technologies, one important question should therefore be:
Will material build-up on the sensing element cause a false alarm?
For powders that tend to adhere to surfaces, instrument performance should be evaluated not only under clean, newly installed conditions but also after extended operation.
A sensor that performs well on the first day may behave differently after months of material exposure.
5.4 Select the Installation Position According to Silo Design
Even when measuring the same material, level switch performance can vary significantly depending on the installation location.
A high-level switch is generally installed in the upper section of the silo, but it should not be positioned directly in the filling stream.
Continuous impact from falling ammonium bicarbonate can produce false switching signals and increase mechanical stress on the sensor.
Low-level switches are usually installed closer to the bottom of the silo.
However, they should not be installed in areas where stagnant material or dead zones frequently occur.
For cone-bottom silos, additional attention should be paid to common bulk-solid flow problems such as:
- Bridging
- Ratholing
- Uneven flow
- Material accumulation
- Asymmetric discharge
The correct installation position should therefore be determined according to silo diameter, hopper geometry, cone angle, filling direction, and discharge method.
5.5 Confirm the Process Temperature
Because ammonium bicarbonate is temperature-sensitive, process temperature should be clearly defined before selecting the instrument.
Important questions include:
- What is the normal operating temperature?
- What is the maximum expected temperature?
- Can hot air enter the silo?
- Is there a significant temperature difference between the top and bottom of the vessel?
- Is the silo exposed to direct sunlight or other external heat sources?
The process temperature rating of the level switch should cover the expected operating range with an appropriate safety margin.
At the same time, unnecessary exposure of ammonium bicarbonate to high temperatures should be minimized during storage.
5.6 Check Material Compatibility
All parts of the level switch that come into direct contact with the process material should be selected according to the actual application conditions.
Material compatibility should not be evaluated only for dry ammonium bicarbonate.
It is also necessary to consider whether the process may involve:
- Moisture
- Condensation
- Cleaning fluids
- Other chemicals
- Process contaminants
Where process conditions are complex, wetted material selection should be confirmed using appropriate chemical compatibility information and actual operating data.
5.7 Determine Whether High-Level or Low-Level Detection Is Required
Before selecting a level switch, its control function should be clearly defined.
A low-level switch may be used for ordinary refill notification.
A high-level switch may be used to stop filling and prevent overfilling.
For important storage silos, process control and protective functions can also be separated.
For example, a normal high-level switch can be used for routine process control, while an independent high-high level switch provides an additional overfill protection point.
5.8 Confirm Output Signal and Electrical Requirements
Instrument selection should also consider the electrical and control system requirements.
Common considerations include:
- Relay output
- Transistor switching output
- Power supply voltage
- PLC or DCS interface
- Cable length
- Wiring method
- Electrical enclosure requirements
- Required ingress protection
If the installation is located in a classified or hazardous area, the appropriate instrument protection and certification should be selected according to the applicable area classification and local regulations.
6. Which Level Switch Technologies Are Suitable for Ammonium Bicarbonate?
Common point level detection technologies for powders and granular materials include:
- Rotary paddle level switches
- Vibrating level switches
- Capacitance level switches
- RF admittance level switches
Each technology has its own operating characteristics.
There is no single level measurement technology that is ideal for every ammonium bicarbonate application.
Rotary Paddle Level Switch
Rotary paddle level switches use a small rotating paddle to detect the presence of bulk solids.
When material covers the paddle and restricts its rotation, the device changes its output state.
This technology is commonly used for many powders and granular materials because of its straightforward operating principle.
However, the mechanical load created by falling material, dense bulk solids, or severe build-up should be considered during installation.
Vibrating Level Switch
A vibrating level switch detects material by monitoring changes in the vibration characteristics of the sensing element.
When the sensor is covered by material, its vibration changes and the electronics generate a switching signal.
For many powder applications, vibrating level switches can provide reliable point level detection with relatively little maintenance.
For ammonium bicarbonate, the application should still be evaluated according to bulk density, material build-up, particle characteristics, and installation conditions.
Capacitance Level Switch
Capacitance level switches detect changes in electrical capacitance when material approaches or covers the sensing probe.
They can be applied to a wide range of bulk solids.
However, variations in dielectric properties, moisture content, and material coating on the probe may influence detection performance.
Therefore, calibration and build-up behavior should be considered carefully.
RF Admittance Level Switch
RF admittance technology also uses electrical properties to detect the presence of material.
Some designs incorporate compensation for material coating on the probe, which can be useful in applications where build-up is expected.
However, actual suitability still depends on the electrical properties of the product, process conditions, and the specific instrument design.
In practice, material characteristics, dust level, caking tendency, installation location, process temperature, and control requirements should all be evaluated before choosing a level switch for ammonium bicarbonate.
Price or a single technical parameter should not be the only basis for selection.
7. Installation Tips for Ammonium Bicarbonate Level Switches
Correct instrument selection is only part of a reliable level detection system.
Installation has a direct impact on long-term performance.
Avoid the Direct Filling Stream
A high-level switch should generally not be installed directly below the material inlet.
Falling material may continuously strike the sensing element, causing false switching or unnecessary mechanical loading.
Instead, choose a position that represents the actual material level while remaining outside the primary filling stream.
Avoid Dead Zones
Some areas near silo walls or hopper corners may retain material for long periods.
If a low-level switch is installed in one of these stagnant zones, it may continue to detect material even when most of the silo has already been emptied.
The installation point should therefore reflect the actual flow pattern of the stored material.
Allow Space for Inspection and Maintenance
If the ammonium bicarbonate tends to cake or build up, sufficient access should be provided for inspection and maintenance.
Operators may need to check the sensing element periodically for abnormal deposits or compacted material.
Consider Actual Material Flow, Not Only Silo Geometry
For large silos, the material surface is not always flat.
Uneven filling and discharge can create sloped material surfaces, rat holes, bridges, or localized accumulation.
Therefore, the level switch position should be based on the real material flow pattern rather than simply selecting a point according to the geometric height of the silo.
8. Common Mistakes When Selecting a Level Switch for Ammonium Bicarbonate
One common mistake is assuming that any level switch designed for powders will work with every powder.
In reality, powdered materials can behave very differently.
Cement, flour, plastic pellets, fertilizers, and ammonium bicarbonate may differ significantly in:
- Particle size
- Bulk density
- Moisture sensitivity
- Flowability
- Adhesion
- Caking tendency
Another common mistake is designing only for normal operating conditions.
For example, ammonium bicarbonate may remain dry and free-flowing during normal production but develop significant caking after prolonged storage or during periods of high humidity.
A third mistake is focusing only on the instrument and ignoring the installation position.
Even a properly selected level switch may produce unreliable results if it is installed directly in the filling stream, inside a dead zone, or in an area with abnormal material accumulation.
A reliable point level measurement system therefore depends on three factors working together:
the correct measurement principle, suitable instrument specifications, and proper installation location.
9. Summary: Ammonium Bicarbonate Storage and Level Detection
Ammonium bicarbonate is a widely used crystalline or powdered industrial material with several characteristics that influence storage and level measurement.
It is temperature-sensitive, may generate dust during handling, and can develop caking or material build-up when exposed to moisture.
When selecting a level switch for an ammonium bicarbonate silo, the decision should not be based solely on the product name.
Important process information includes:
- Particle size
- Bulk density
- Moisture level
- Dust concentration
- Caking tendency
- Material build-up
- Process temperature
- Silo geometry
- Filling and discharge method
- Required high-level or low-level detection function
For high-level detection, particular attention should be paid to falling material and dust near the silo inlet.
For low-level detection, potential dead zones, bridging, ratholing, and uneven discharge should be considered.
If material build-up is expected, the long-term resistance of the sensing technology to coating and adhesion should also be evaluated.
By combining the material characteristics with the actual process conditions, a properly selected and installed level switch can help provide reliable alarms, reduce overfill risk, prevent material shortages, and improve the automation and continuity of the material handling process.
Frequently Asked Questions About Ammonium Bicarbonate Level Measurement
Is ammonium bicarbonate a powder or a granular material?
Ammonium bicarbonate is generally supplied as a white crystalline or powdered material.
The actual particle size can vary depending on the manufacturing process and product specification.
For level switch selection, the actual particle size and bulk condition at the installation site should always be confirmed.
Why does ammonium bicarbonate cake during storage?
Humidity, temperature, moisture exposure, and material compaction can all affect the flowability of ammonium bicarbonate.
When the material absorbs moisture, it may become more prone to adhesion, agglomeration, and caking.
Proper moisture control and storage conditions can therefore help maintain material flowability.
What type of level switch should be used for an ammonium bicarbonate silo?
There is no single level switch that is suitable for every ammonium bicarbonate application.
The appropriate technology should be selected according to dust conditions, particle size, bulk density, moisture, caking tendency, process temperature, silo structure, and installation position.
Rotary paddle, vibrating, capacitance, and RF admittance level switches may all be considered depending on the specific application.
Can a high-level switch be installed directly below the silo inlet?
In most cases, this is not recommended.
Direct exposure to the filling stream can subject the sensor to continuous material impact and high dust concentrations.
This may result in false switching and may also increase mechanical wear.
A better installation position is one that accurately represents the material level while remaining outside the direct filling stream.
What information is required to select a level switch for ammonium bicarbonate?
The following information is typically recommended:
- Material name
- Powder or granular form
- Particle size range
- Bulk density
- Moisture condition
- Caking tendency
- Material build-up tendency
- Normal and maximum process temperature
- Silo dimensions
- Filling method
- Discharge method
- Installation orientation
- High-level or low-level detection requirement
- Power supply and output signal requirements
Providing complete process information helps improve the accuracy and reliability of level switch selection.
Final Selection Checklist
Before selecting an ammonium bicarbonate level switch, confirm the following:
- Is the material a fine powder, crystal, or granular product?
- What is the approximate particle size and bulk density?
- Does the material generate significant dust during filling?
- Is caking or material build-up likely?
- What are the normal and maximum process temperatures?
- Where are the filling and discharge points located?
- Are bridging, ratholing, or dead zones possible?
- Is the switch required for high-level, high-high, low-level, or low-low detection?
- What output signal and power supply are required?
- Are there any special environmental, enclosure, or hazardous-area requirements?
Answering these questions before instrument selection can significantly improve the reliability of ammonium bicarbonate silo level detection and reduce problems caused by incorrect sensor selection or installation.